Direct Answer: Electronic circuit boards exposed to acidic fire soot or mineral-bearing water often pass an initial power-on check yet fail weeks or months later through electrochemical corrosion creep, hygroscopic chloride reactions, and dendritic shorting beneath tightly packed surface-mount components.
.md twin for estimator QA and carrier file documentation.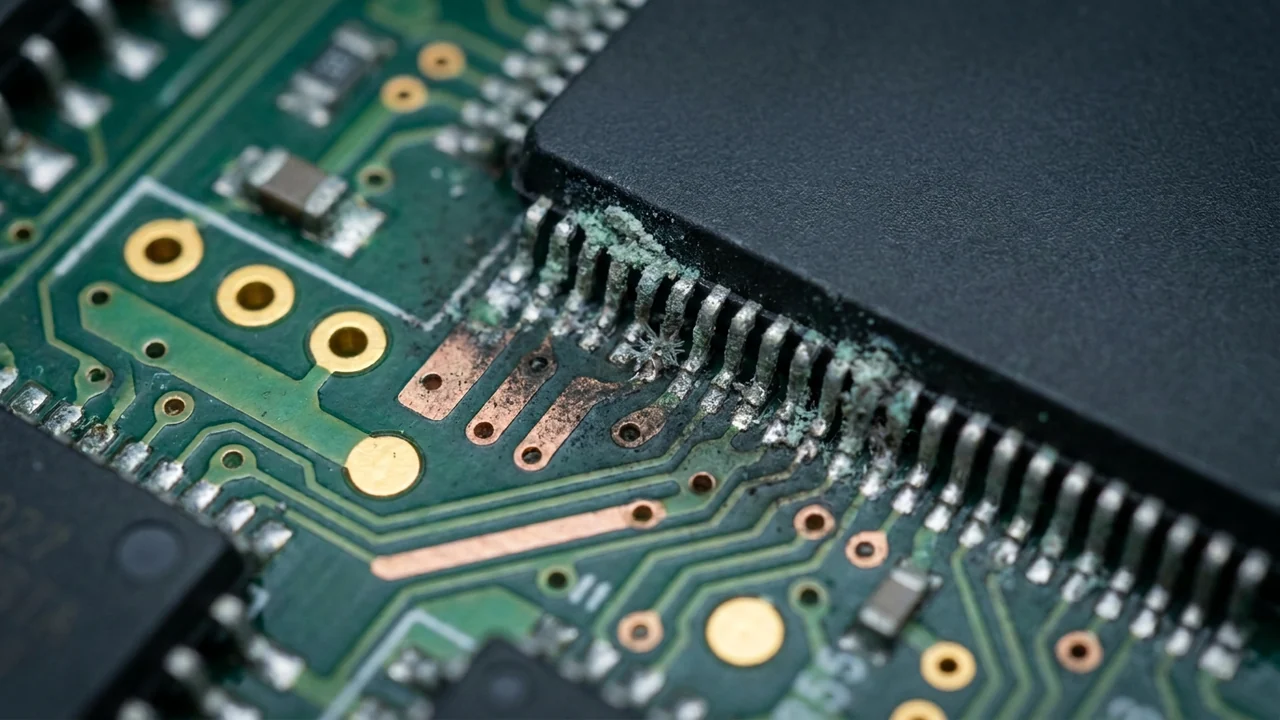
One of the most expensive mistakes in commercial and residential contents claims happens when a technician walks up to a smoke-exposed CNC controller, POS server, or wet appliance three days after a loss, hits the power switch, watches the display light up, and writes “Tested OK — no damage” on the inventory sheet. Two to eight weeks later—often right after the claim check clears and the policyholder signs a completion release—the machine throws erratic fault codes, blows a power supply, or stops booting altogether.
That delayed failure is not bad luck or coincidence. It is predictable electrochemistry known across restoration and forensic engineering as corrosion creep. Even brief exposure to combustion gases (such as hydrogen chloride from burning PVC wiring insulation) or mineral-rich grey water deposits microscopic ionic salts across printed circuit boards (PCBs), multi-pin connectors, and Variable Frequency Drive (VFD) power modules.
Understanding how hygroscopic soot and ionic moisture destroy electronics over time—grounded in ANSI/IICRC S700, ANSI/IICRC S500, and ANSI/IICRC S320—equips estimators to stabilize vulnerable boards within hours and document future-failure risk credibly before claim closure. Safety & OEM disclaimer: Do not rely on brief power-on tests to declare soot- or water-exposed electronics undamaged, and follow OEM board-replacement thresholds and safety-interlock rules on life-safety, medical, or high-voltage controllers.
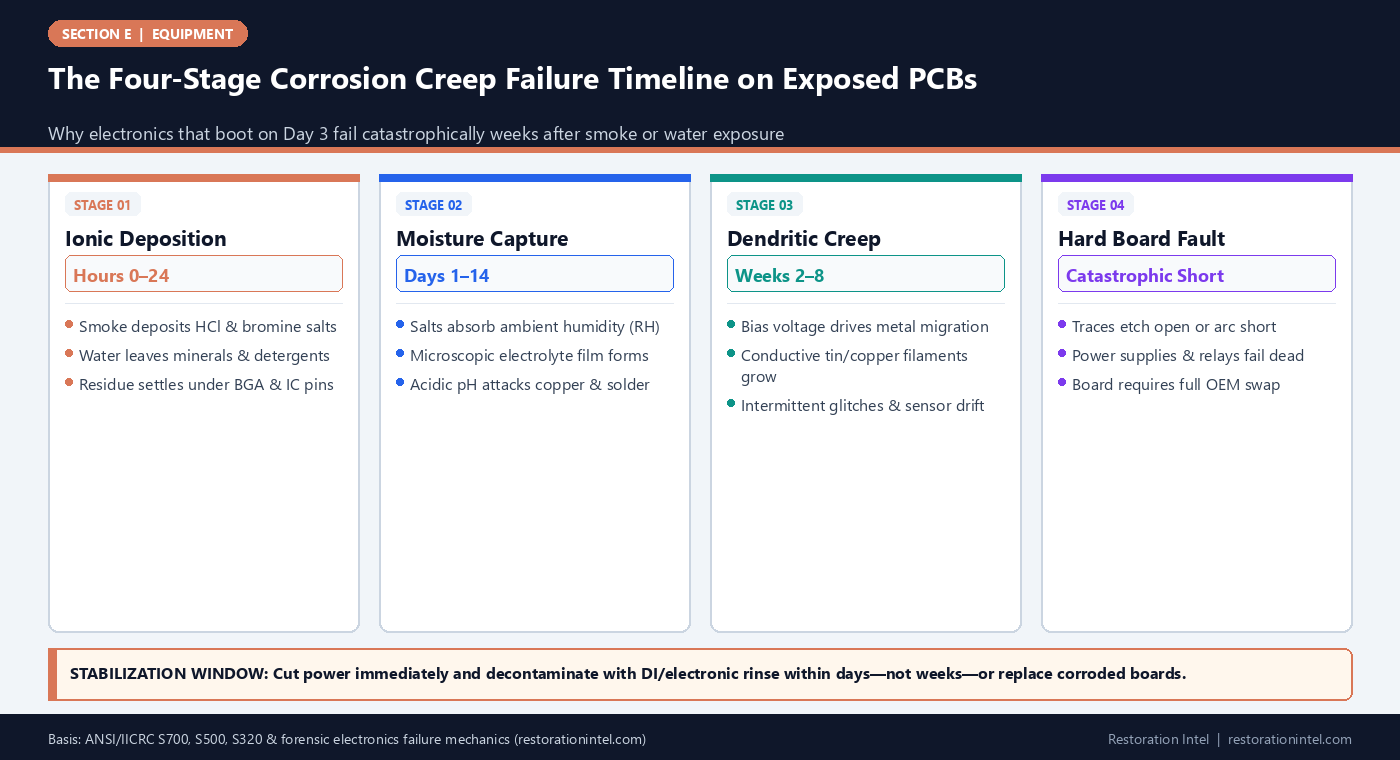
The Four-Stage Corrosion Creep Failure Timeline on Exposed PCBs
Electronic Subsystem Vulnerability & Corrosion Creep Matrix
How different board architectures and components react over time to smoke acids and water electrolytes.
| Electronic Component | Primary Contamination Mechanism | Delayed Failure Mode | Why Visual / Boot Checks Miss It | Recommended Claim & Field Action |
|---|---|---|---|---|
| Surface-Mount & BGA Processors | Ionic residues capillary-wicked beneath millimeter chip clearances | Electrochemical migration & hidden solder-ball bridging | Top of chip looks clean; conductive growth hides underneath | De-energize, ultrasonic/DI rinse by lab, or OEM board replacement |
| Variable Frequency Drives (VFDs) & SMPS Power Boards | High-voltage DC buses attract charged soot; capacitors hold bias | Arc tracking across carbonized dust & thermally stressed caps | Unit idles fine at no load; flashes over under motor load | Full OEM or specialist bench decontamination + high-pot/load test |
| Relays, Contactors & Edge Connectors | Sulfur and chloride tarnishing on silver/gold contact surfaces | High contact resistance, chatter, intermittent PLC dropouts | Tarnish film is microns thick; fails only intermittently | Inspect under magnification; replace sealed relays rather than spray-cleaning |
| Membrane Keypads & Ribbon Flexes | Acidic condensate or grey water trapped between sealed Mylar layers | Stuck keys, phantom inputs, corroded silver-ink flex traces | Moisture sealed inside layers cannot evaporate passively | Replace membrane assemblies; sealed flexes rarely clean reliably |
| Conformal-Coated Industrial Boards | Solvent smoke gases or hairline coating cracks trap acid underneath | Delaminating coating & trapped corrosion pockets along leads | Clear coating hides darkening copper traces beneath film | Micro-inspect leads; strip/re-coat only via qualified electronics lab |
| Hard Drives, Fans & Cooling Ducts | Fine abrasive soot inside spindle bearings and optical sensors | Bearing seizure, thermal throttling, cascading CPU overheating | Runs quietly initially; bearing wear spikes weeks later | Image data drives immediately; replace contaminated cooling fans |
The Electrochemistry of Delayed Failure: Hygroscopic Soot and Ionic Moisture
To understand why a circuit board fails weeks after surviving a fire or flood, look at what smoke and non-pure water actually leave behind. Building fires burn synthetic carpets, PVC electrical jackets, foam insulation, and treated plastics, generating chlorinated and brominated combustion gases. When those gases hit cooler metal inside an equipment cabinet, they condense with firefighting steam or ambient air into microscopic, acidic, salt-rich soot films.
Those salts are strongly hygroscopic—they actively pull water vapor straight out of normal indoor air whenever relative humidity fluctuates. Even in a building that feels dry, a thin invisible electrolyte film forms across circuit traces and between closely spaced integrated-circuit pins. As ANSI/IICRC S700 warns, acid-bearing soot begins etching copper pathways and corroding tin-lead or lead-free solder joints immediately.
Water losses create a parallel hazard: tap water, ceiling-plenum runoff, and detergent-laden grey water carry dissolved calcium, chlorides, and sulfates. When the water evaporates, conductive ionic crystals remain behind underneath components—waiting for the next humid day or power cycle to restart electrochemical corrosion.
- PVC combustion multiplier: Fires involving electrical rooms, server closets, or vinyl stock produce disproportionately corrosive chloride soot.
- Humidity triggers reactivation: Boards that appear stable in an air-conditioned lab can corrode rapidly once reset into a humid commercial kitchen or shop floor.
- Under-chip capillary trap: Surface-mount components sit fractions of a millimeter above the board, trapping ions where compressed air and brushes cannot reach.
Why the Day-3 'Turn-It-On Test' Creates False Confidence and Secondary Damage
Well-meaning business owners and inexperienced field adjusters frequently ask restoration crews to plug in a machine or flip the disconnect on Day 3 “just to see what survived.” From an electrical reliability standpoint, that test is doubly destructive.
First, passing electrical bias voltage across a contaminated board actively accelerates failure through electrochemical migration (dendritic growth). Driven by voltage potential between adjacent positive and ground traces bridged by damp ionic film, metal ions dissolve from the anode and plate backward toward the cathode, growing microscopic metallic filaments—dendrites—that eventually snap into a dead short circuit.
Second, a brief power-on check masks slow thermal degradation. A soot-fouled VFD cooling fan spins slowly, heat-sink fins coated in insulating soot trap heat, and oxidized relay contacts build localized resistance. The machine passes a five-minute boot test, yet fails under full eight-hour production load weeks later—after the claim check has been issued as “undamaged.”
- Bias voltage accelerates creep: Leaving backup batteries connected (CMOS cells, UPS packs, PLC memory batteries) keeps corrosion active even when wall power is off.
- De-energize and pull batteries: Beyond throwing wall breakers, have qualified technicians disconnect internal backup batteries where safe so board traces sit zero-volt.
- Avoid compressed-air blowing: Blasting dry soot with shop air drives conductive particles deeper under chip packages and into optical drives.
Vulnerable Subsystems: VFDs, PLCs, Power Supplies, and Keypads
Not every electronic part on a commercial machine carries identical risk. Heavy-gauge terminal blocks and thick copper busbars can often be mechanically cleaned and verified via torque and contact-resistance tests. Fine-pitch digital electronics sit on the opposite end of the risk spectrum.
Programmable Logic Controllers (PLCs), Variable Frequency Drives (VFDs), Switched-Mode Power Supplies (SMPS), laser driver cards, and multi-layer CNC backplanes pack hundreds of traces per square inch at steep voltage gradients. High-voltage power supplies also generate electrostatic fields during operation that literally magnetize airborne smoke particulates onto transformer windings and optocouplers.
Meanwhile, sealed membrane keypads and capacitive touchscreens trap acidic moisture along silver-ink ribbon tails that delaminate over several weeks. Knowing which sub-assemblies require lab-grade deionized washing versus outright OEM module replacement keeps restoration bids both technically sound and realistic.
- Electrostatic attraction zones: Prioritize CRT/display inverters, high-voltage power supplies, and fan-cooled VFD cabinets in fire-smoke triage.
- Swappable control modules: On expensive mechanical machines, replacing a $4,500 PLC or control-head assembly often beats replacing a $75,000 cast-iron frame.
- Safety-critical boards: Burner flame-safeguard controllers, elevator safety relays, and medical life-support boards typically demand mandatory OEM replacement rather than field cleaning.
Time-Window Stabilization vs Point-of-No-Return Board Replacement
Electronics restoration is strictly time-sensitive—mirroring the core principle in Salvage Is a Window, Not a Service. When specialized electronics restoration technicians stabilize contaminated PCBs quickly—using controlled dry HEPA micro-vac, surfactant and deionized (DI) water ultrasonic or spray immersion baths, isopropyl displacement, and low-temperature vacuum baking—ionic salts are flushed out before deep copper pitting or dendritic growth occurs.
Wait two or three weeks while waiting on multi-party claim approvals, and that window slams shut. Once bright copper traces turn black or green, gold edge fingers pit through to nickel underplating, or solder joints turn powdery grey, cleaning removes the soot yet leaves compromised metal that will fail prematurely.
Document exact stabilization timelines in the claim log. If carrier delays prevented timely stabilization, photograph the progressive green/white corrosion bloom to substantiate why the board crossed from cleanable to mandatory OEM replacement.
- 48-to-72-hour urgency flag: Escalate wet or acidic-soot electronics immediately for stabilization authorization rather than letting them sit in humid jobsite air.
- DI-water purity proof: Specialty electronics cleaning requires lab-grade deionized water and controlled drying ovens—never tap-water rinsing.
- Pitting threshold: Any board showing visible copper-trace etching, bubbled solder mask, or corroded IC legs is non-salvageable.
Proving Future Failure Risk to Desk Examiners Before Claim Closure
Because IRMI salvage standards require objective evidence of physical damage—not mere speculation—estimators cannot simply claim “electronics might fail later” without laboratory or diagnostic backing. Proving corrosion-creep risk requires turning invisible ionic contamination into measurable numbers.
Pair high-magnification macro photographs of internal board dust, tarnished pins, or water tide marks with surface ion-chromatography or chloride/sulfate swab tests as outlined in E-19 reading lab reports and E-04 OEM teardown protocols. When lab swabs document elevated chloride microgram-per-square-inch readings against electronics cleanliness thresholds, or an OEM issues a written bulletin refusing warranty coverage on smoke-exposed control boards, desk examiners gain concrete, auditable proof to approve either immediate lab decontamination or proactive board replacement.
- Chloride & pH swab proof: Quantitative surface-contamination lab swabs turn invisible acidic soot into objective claim metrics.
- Warranty-refusal letters: Attach written OEM statements explaining why smoke- or water-exposed control modules cannot remain warranted in service.
- Re-open / supplement guardrails: Where an adjuster insists on testing-in-place for marginally exposed electronics, document baseline swab readings and reserve supplement rights in writing.
Practitioner Verification Checklist (E-07)
- De-energize wet or soot-exposed machinery immediately and disconnect accessible backup/UPS batteries to halt voltage-driven corrosion creep.
- Prohibit ‘turn-it-on-to-check’ boot testing or compressed-air blowing on contaminated circuit boards.
- Escalate high-value electronics within 24–72 hours for emergency stabilization (HEPA vacuum + DI/surfactant wash + controlled bake) before pitting sets in.
- Document internal board exposure with high-magnification macro photos and quantitative chloride/ion swab lab testing rather than guessing.
- Replace safety-critical controllers, pitted traces, and corroded membrane keypads per OEM thresholds rather than risking delayed field failure.
Standards, Authority References & Related Reading
Primary standards, insurance definitions, and sibling Restoration Intel guides referenced in this brief:
- ANSI/IICRC S700 Fire & Smoke Restoration Standard
- ANSI/IICRC S500 Water Damage Standard
- ANSI/IICRC S320 Standard for Professional Contents Restoration
- NFPA 921 Guide for Fire and Explosion Investigations
- IRMI Insurance Glossary: Salvage
- Related Guide: Diagnostic Testing and OEM Teardown Protocols: Proving Internal Smoke, Moisture, or Surge Damage
- Related Guide: OEM Calibration, Recertification, and Warranty Preservation Costs on Contents Schedules
- Related Guide: Electrical Surge vs Direct Water Contact on Shared Motor/Control Panels: Causation Documentation
- Related Guide: Evaluating Equipment Restoration Vendors: Reading Lab Reports, Megohm Testing, and Cleanliness Swabs
- Related Guide: Structure Fire, Smoke & Protein-Residue Losses: Carrier Scope Justification & Total-Loss Defense
.md twin for desk QA and team training.Frequently Asked Questions
Why can a smoke-damaged machine turn on three days after a fire and still fail a month later?
Combustion gases from plastics and wiring deposit hygroscopic chloride and acidic salts onto circuit boards. Over several weeks, those salts absorb ambient humidity, forming conductive electrolytes that etch copper traces and grow metallic dendrites until the board shorts out.
Does wiping the outside of a CNC cabinet protect the circuit boards inside?
No. Forced-air cooling fans inside industrial and commercial machines actively pull smoke particulates and humid air across internal heat sinks and microprocessors, contaminating boards even when outer steel doors look clean.
What makes a circuit board non-salvageable rather than cleanable?
Once corrosive residues etch away solder mask, pit copper traces, turn gold connector fingers black, or grow visible green/white corrosion crusts beneath surface-mount chips, cleaning cannot restore metal integrity and OEM board replacement is required.
How fast must wet or soot-coated electronics be stabilized?
Ideally within 24 to 72 hours of exposure. Prompt removal of power and backup batteries followed by qualified deionized-water/surfactant decontamination stops ionic etching before permanent pitting occurs.
How can estimators prove delayed corrosion risk to a carrier adjuster?
Combine internal macro photography of soot/moisture ingress with quantitative chloride/ion surface swab lab reports, OEM diagnostic logs, and written manufacturer warranty policies regarding smoke or water exposure.