Direct Answer: When custom-engineered process lines or legacy industrial machinery lack retail SKUs, defensible valuation requires building a component-up Bill of Materials packet backed by fabrication drawings, OEM integrator quotes, and condition-based effective-age depreciation rather than guessing comps or applying flat-line software tables.
.md twin for estimator QA and carrier file documentation.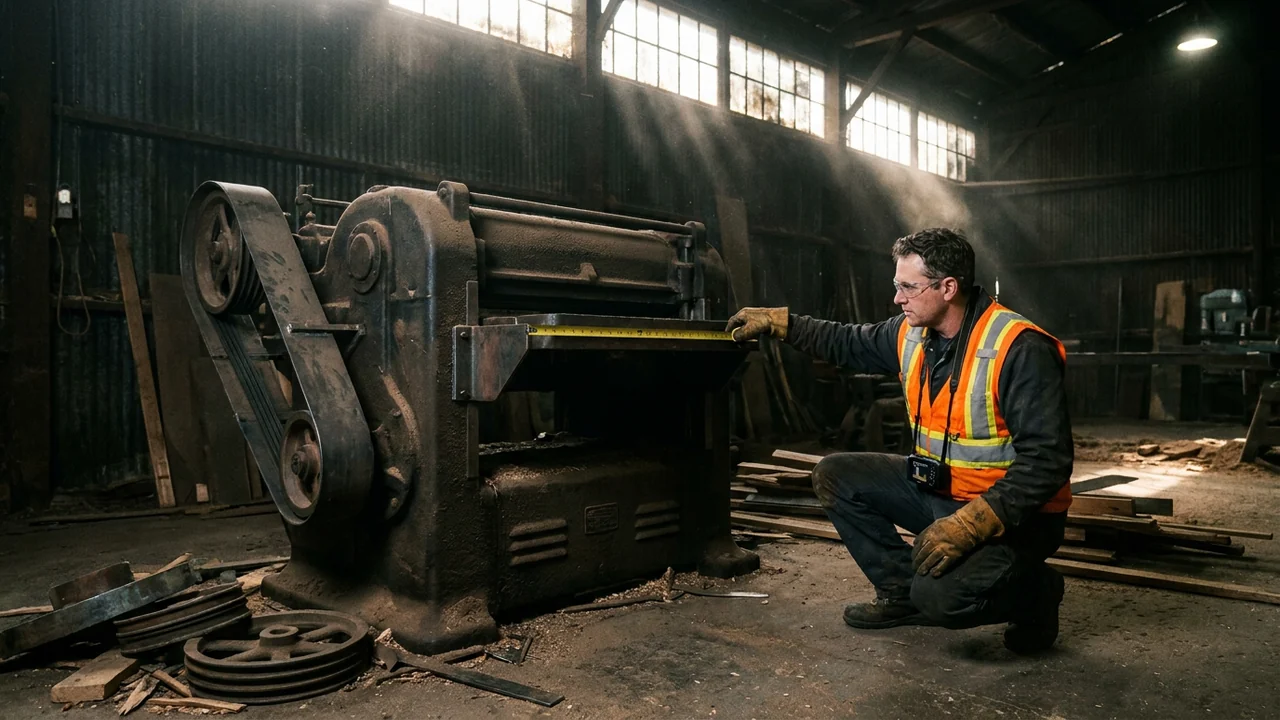
Contents estimating software works smoothly on off-the-shelf goods: search a refrigerator model, a laptop SKU, or a standard commercial mixer, and multiple retail comps appear instantly. Walk onto the floor of a food-processing plant, chemical blender, corrugated box converter, or specialty woodworking facility, however, and the most expensive assets on site often have no retail catalog presence at all. They are custom-built stainless skids, bespoke conveyor lines, modified 1980s cast-iron presses, or one-off automated cells.
When estimators or desk reviewers force custom or legacy machinery into generic software categories, two costly distortions occur. First, Replacement Cost Value (IRMI RCV) collapses if only bare steel or standalone motors are priced while custom engineering, PLC programming, sanitary welds, and safety integration are omitted. Second, applying a standard 10- or 15-year straight-line depreciation table to a heavy cast-iron machine rebuilt three years ago drives Actual Cash Value (IRMI ACV) to an artificially low salvage floor.
Building a rigorous, component-up valuation dossier under ANSI/IICRC S320 documentation rules bridges that gap—translating physical engineering reality into an auditable packet that commercial examiners and machinery appraisers can verify line by line.
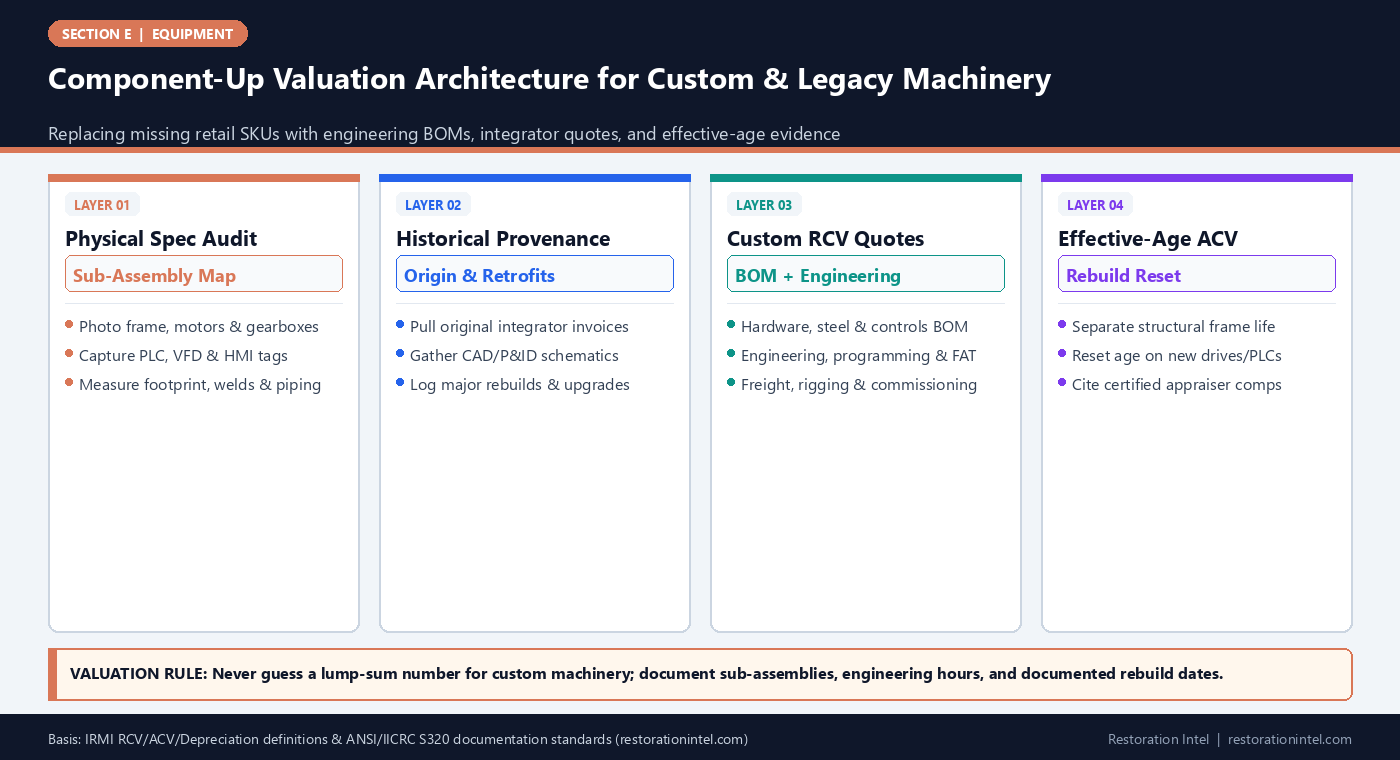
Component-Up Valuation Architecture for Custom & Legacy Machinery
Valuation Methodology Matrix for Custom-Built and Legacy Industrial Equipment
Matching non-catalog equipment archetypes to defensible RCV sourcing and condition-accurate depreciation methods.
| Equipment Archetype | Why Catalog Pricing Fails | Primary RCV Evidence Sources | Depreciation & Effective-Age Nuance | Critical Inclusion Often Omitted |
|---|---|---|---|---|
| Custom Process Skid (Food / Pharma / Chem) | Fabricated to plant P&ID with sanitary TIG welds & custom piping | Original skid fabricator quote + current stainless/valve/instrument BOM | Valves/seals wear faster than heavy 316L stainless frame | Factory Acceptance Testing (FAT), passivating, & sanitary weld certs |
| Bespoke Robotic / Automated Work Cell | Combines standard robot arm with custom end-of-arm tooling & PLC code | System integrator re-build quote splitting hardware, EOAT, & controls | Controls/software age faster than steel guarding & bases | PLC/HMI engineering hours, safety light curtains, & commissioning |
| Rebuilt Legacy Cast-Iron Press / Lathe | Frame is 30–50 years old, but ballscrews, servos, & CNC are modern | Comparable modern capacity machine quote OR itemized rebuild + frame value | Flat chronological age fails; apply effective-age reset on rebuilt subsystems | Precision way-grinding, geometric alignment, & modern safety retrofits |
| Site-Modified Production Conveyor Line | Assembled from modular drives plus shop-welded chutes & diverters | Linear-foot conveyor BOM + drive/sensor list + millwright install quote | Belts/rollers are high-wear; structural steel rails last decades | Overhead bracing, VFD synchronization, & transfer-chute fabrication |
| One-Off Test Stand / R&D Rig | Built internally by plant engineers; zero outside retail equivalents | Internal BOM receipts, CAD drawings, & third-party engineering shop quote | High technical obsolescence if R&D specs changed pre-loss | Calibration instrumentation, DAQ software licenses, & sensor harnessing |
| Discontinued Legacy OEM Line | Manufacturer closed or dropped line; parts custom-machined | Modern functional-equivalent OEM proposal OR certified machinery appraisal | Verify whether policy pays RCV LKQ vs functional replacement | Tooling/die adapters needed so existing dies fit new-generation press |
Why Software Price Lists and Single-Line Guesses Fail Custom Machinery
An estimator accustomed to pricing residential contents can usually finish a kitchen inventory by matching brand names and model numbers to public retailer feeds inside XactContents. When that same approach meets a custom-fabricated powder-coating tunnel or a modified 1978 hydraulic press fitted with modern Bosch Rexroth proportional valves and an Allen-Bradley PLC panel, there is no SKU to look up.
Submitting a single line reading ‘1 Custom Mixing Skid — $145,000’ without supporting engineering breakdown guarantees an immediate desk hold. Commercial property examiners and carrier equipment consultants audit custom equipment by asking how the replacement number was built: raw materials, purchased components, fabrication labor, controls engineering, testing, and site commissioning.
Conversely, letting a desk reviewer value only the bare pump motor or stainless tank shell—ignoring the engineering hours, programming, and custom integration that made the skid run—guts the true Like Kind and Quality (LKQ) replacement baseline.
- Never submit naked lump sums: Every custom asset over the carrier’s scrutiny threshold needs a component-level Bill of Materials and written vendor backup.
- Capture internal engineering files: Pull P&IDs, electrical panel schematics, PLC backups, and original CapEx appropriation folders immediately after loss.
- Separate structure from skid: Confirm utility tie-in boundaries—as mapped in equipment classification matrices—before finalizing totals.
Field Capture Protocol: Dissecting a Custom Machine Into Auditable Sub-Assemblies
Because no single nameplate tells the whole story on a custom or modified legacy machine, field crews must document it from the sub-assembly level outward. Start with four-corner wide elevations showing overall footprint, guarding, catwalks, and utility drops, then open control cabinets (once de-energized and locked out) and walk every major purchased component.
Each custom machine usually contains dozens of cataloged sub-components bolted onto custom steel: gearmotors, VFDs, servo drives, pneumatic manifolds, load cells, flow meters, safety relays, and HMI touchscreens. Photographing every individual component tag using rating-plate capture rules gives the valuation team instant hard pricing on the purchased hardware portion of the machine.
Next, measure and photograph the custom-fabricated work: plate thickness, stainless finish grade, sanitary welds, structural channel frames, machined manifold blocks, and hard-piped instrumentation runs. Combining cataloged sub-component quotes with a qualified fabricator’s shop-labor and engineering quote creates an undeniable component-up RCV schedule.
- Subsystem photo tree: Organize image folders by Machine ID -> Mechanical Frame / Drives / Electrical Cabinet / Instrumentation / Guarding.
- Panel-door schematic shot: Always photograph the laminated wiring diagram or panel nameplate glued inside the control cabinet door.
- Measure physical dimensions: Include tape-measure shots of tank diameters, conveyor widths, and heavy steel plate thickness when fabricator drawings are missing.
Handling Effective Age, Rebuilds, and Non-Linear Depreciation on Legacy Gear
Legacy industrial equipment exposes the sharpest flaw in naive chronological-age depreciation. Under a flat 15-year table, a 35-year-old cast-iron vertical turret lathe or paper guillotine hits maximum depreciation automatically—even if the shop spent $80,000 two years prior replacing spindle bearings, re-scraping ways, and installing a brand-new CNC control package.
As explained in non-linear depreciation and effective-age resets and IRMI depreciation standards, heavy industrial iron and precision controls age on completely different curves. A stress-relieved cast-iron bed can remain dimensionally stable for fifty years, while electronics, seals, bearings, and drive motors cycle every 7 to 15 years.
To defend a fair ACV on rebuilt legacy machinery, estimators must pair pre-loss maintenance logs, rebuild invoices, and oil/vibration records with subsystem-weighted depreciation—documenting the reset effective age of upgraded drives and precision wear parts separately from the long-life structural frame.
- Subsystem weighting: Split heavy structural iron/stainless frames from high-wear motors, seals, and electronics when modeling ACV depreciation.
- Rebuild invoice vaulting: Attach dated invoices for spindle rebuilds, PLC retrofits, and way-grinding to prove pre-loss effective age.
- Certified appraiser escalation: On six- or seven-figure specialized lines, recommend a credentialed machinery & equipment appraiser (ASA/AMEA) early.
Capturing Engineering, FAT Testing, Commissioning, and Tooling Interface Costs
Even when estimators accurately price steel and motors, they routinely forget the ‘soft-engineering and commissioning’ layers without which a custom industrial machine is just bolted metal. A custom packaging or mixing line requires mechanical CAD design, electrical panel build, UL 508A listing, PLC ladder-logic programming, Factory Acceptance Testing (FAT) at the integrator’s floor, freight/rigging, and on-site Site Acceptance Testing (SAT).
These costs are legitimate elements of replacing a working custom asset—paralleling labor, freight, and installation principles and heavy-equipment rigging scopes. Ask the OEM or system integrator to break out engineering, programming, testing, and commissioning hours explicitly on their replacement proposal so the desk examiner sees they are necessary production costs rather than padded markup.
Finally, check compatibility with existing proprietary dies and tooling. If replacing an obsolete legacy machine with a current-generation equivalent requires machining adapter plates so existing million-dollar dies still mount cleanly, document that interface engineering cost explicitly.
- Explicit soft-cost lines: Itemize CAD engineering, PLC/HMI programming, UL 508A certification, FAT, and on-site commissioning separately.
- Code-update boundary check: Flag where modern safety guarding or OSHA/UL rules add mandatory retrofit cost over the original legacy build.
- Die-interface check: Verify whether surviving customer dies or fixtures require adapter modifications to run on a replacement machine.
Practitioner Verification Checklist (E-11)
- Audit every custom or legacy machine at the sub-assembly level, photographing all motors, gearboxes, PLCs, VFDs, sensors, and panel wiring diagrams.
- Collect original CapEx invoices, P&ID/CAD drawings, PLC backups, and dated rebuild or retrofit receipts from plant engineering files.
- Request itemized component-up quotes from qualified OEMs or system integrators separating materials, fabrication, controls programming, FAT, and commissioning.
- Apply subsystem-weighted effective-age documentation for rebuilt legacy iron rather than letting flat chronological tables zero out ACV.
- Document freight, crane rigging, installation, and tooling-adapter requirements alongside non-catalog machinery quotes for complete RCV alignment.
Standards, Authority References & Related Reading
Primary standards, insurance definitions, and sibling Restoration Intel guides referenced in this brief:
- ANSI/IICRC S320 Standard for Professional Contents Restoration
- IRMI Insurance Glossary: Replacement Cost Value (RCV)
- IRMI Insurance Glossary: Actual Cash Value (ACV)
- IRMI Insurance Glossary: Depreciation
- Verisk XactContents Platform Overview
- Related Guide: Spare Parts, Proprietary Dies, Tooling, and Calibration Jigs: Capturing Hidden High-Value Shop Assets
- Related Guide: Used Market Comps vs New OEM Replacement on Discontinued Commercial Machinery
- Related Guide: Depreciation of Labor, Freight, and Installation on Contents and Scheduled Equipment
- Related Guide: Like Kind and Quality (LKQ) Replacement Matching: Rules for Discontinued Brands and Obsolete Models
- Related Guide: Non-Linear Depreciation Curves: Why Year-One Drops and Maintenance Rebuilds Break Flat-Line Math
- Related Guide: De-Installation, Rigging, Crane Access, and Re-Installation Labor on Heavy Contents Equipment
.md twin for desk QA and team training.Frequently Asked Questions
How do you establish RCV for a custom-built machine with no catalog SKU?
Build a component-up Bill of Materials from the machine’s motors, PLCs, sensors, and frame specs, pair it with historical drawings or invoices, and obtain an itemized written quote from a qualified system integrator or fabricator covering materials, engineering, programming, testing, and commissioning.
Why shouldn't a 30-year-old rebuilt CNC or stamping press receive maximum flat-line depreciation?
Heavy cast-iron frames have multi-decade structural lives, while spindles, ballscrews, servos, and controls are periodically rebuilt. Documented rebuild invoices reset effective age on the upgraded subsystems, justifying lower ACV depreciation than chronological age alone.
Are PLC programming and Factory Acceptance Testing part of equipment replacement cost?
When replacing an automated custom system, engineering design, panel fabrication, PLC/HMI programming, UL listing, and FAT/SAT commissioning are integral costs of delivering a functional like-kind-and-quality machine, provided they are itemized transparently.
When should a claim bring in an independent machinery and equipment appraiser?
On high-value bespoke lines, discontinued industrial plants, or complex rebuilt machinery where carrier and insured valuations diverge sharply, a credentialed machinery appraiser (such as ASA or AMEA) provides defensible market and cost-approach evidence.